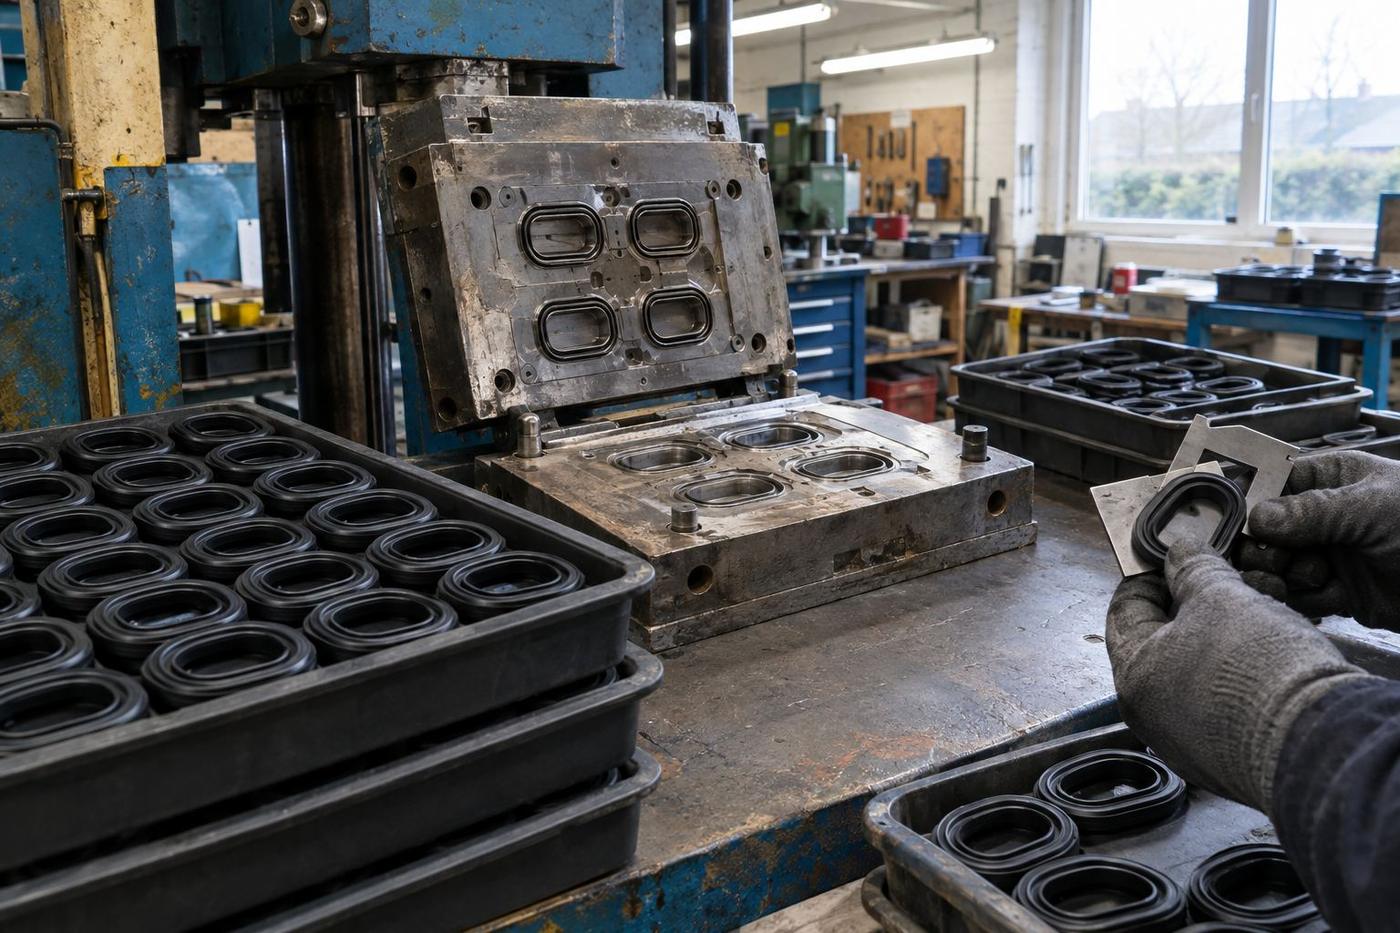
Gasket and seal manufacture
Silicone and rubber gaskets moulded to your drawing, in the grade and hardness your sealing job actually needs. Enclosure gaskets, static fluid…
See the serviceProject record · Automotive tier-2 · Compression
A rubber sealing component supplied into a tier-1 that fits it into a vehicle. Not exotic; not complex; just needs to arrive when the build schedule needs it. That's harder than it sounds.
The brief
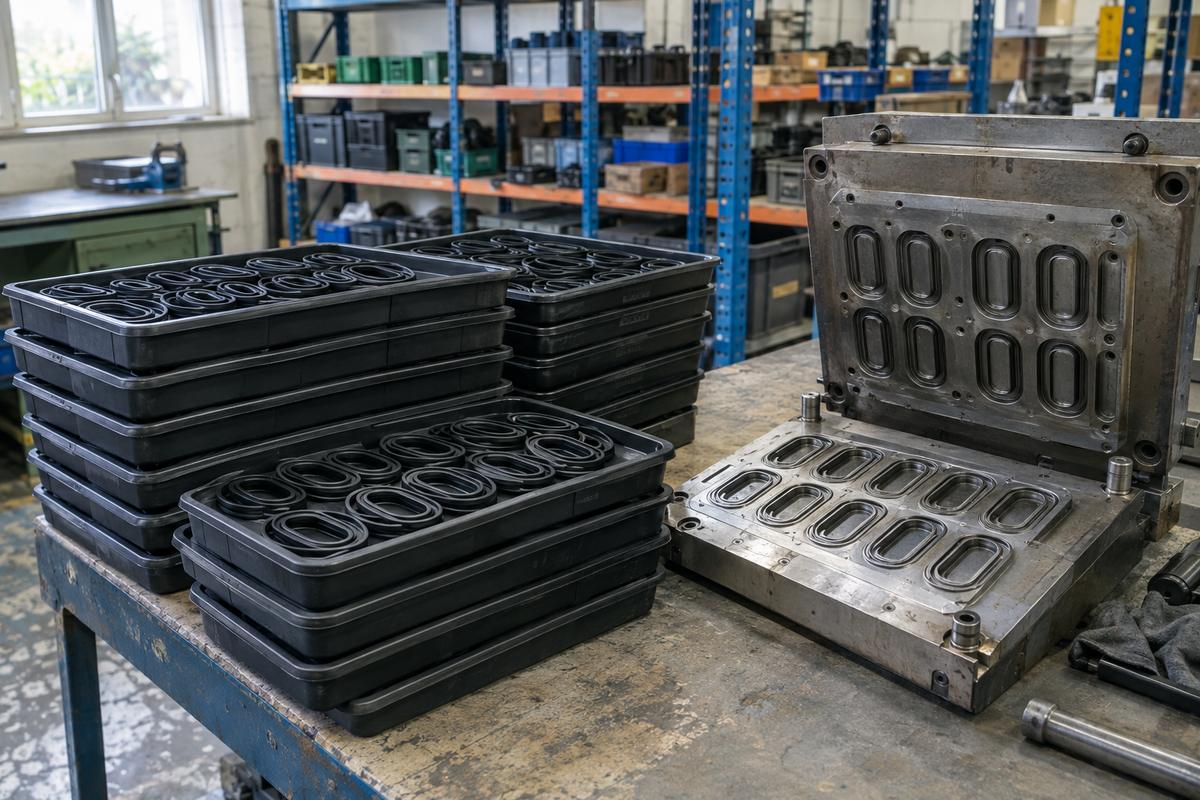
A UK-based tier-2 automotive supplier had been sourcing an EPDM sealing component from a European moulder for several years. The parts were fine. The delivery reliability wasn't. Build schedules from the tier-1 fluctuated week to week; the European supplier's schedule couldn't respond fast enough.
The tier-2 supplier was carrying weeks of safety stock to cover the schedule gap. Working capital tied up in a warehouse; risk of scrap if the tier-1 revised down; exposure if the tier-1 revised up faster than the supplier could react.
They needed UK supply — same part, same material spec, but with lead time that matched the tier-1's cadence. That's why they came to us.
The problem
The part itself needed no design change. It was a straightforward EPDM sealing gasket, compression-moulded, with a spec that the tier-2 already trusted. The problem was the geography and the batch model, not the manufacturing.
We proposed a UK-based programme: we make the tool, we hold stock at a defined buffer level, we produce batches on shorter lead times than the European supplier could match. Payback for the tooling investment would happen through reduced safety stock and reduced lost sales from build-schedule mismatch.
The commercial conversation was less about unit price (roughly comparable to the European supplier) and more about total cost of ownership, factoring in inventory carrying cost and stock-out risk.
What we changed
The manufacturing was standard. The commercial arrangement was where the value was.
Tool built to the existing drawing, first samples matched against retained parts from the European supplier.
EPDM compound verified against the tier-1's original approval documentation. Compound spec locked for the programme.
Not weeks — days. Enough to absorb build-schedule fluctuation without the working capital hit of the previous arrangement.
Batches produced on a defined lead time from PO. UK freight to customer's assembly location.
Rolling forecast reviewed monthly. Buffer level adjusted based on recent volatility. Both sides visible into the same numbers.
Named engineer, escalation path to operations lead, defined response times for urgent orders. Not just an email address.
The commercial shape
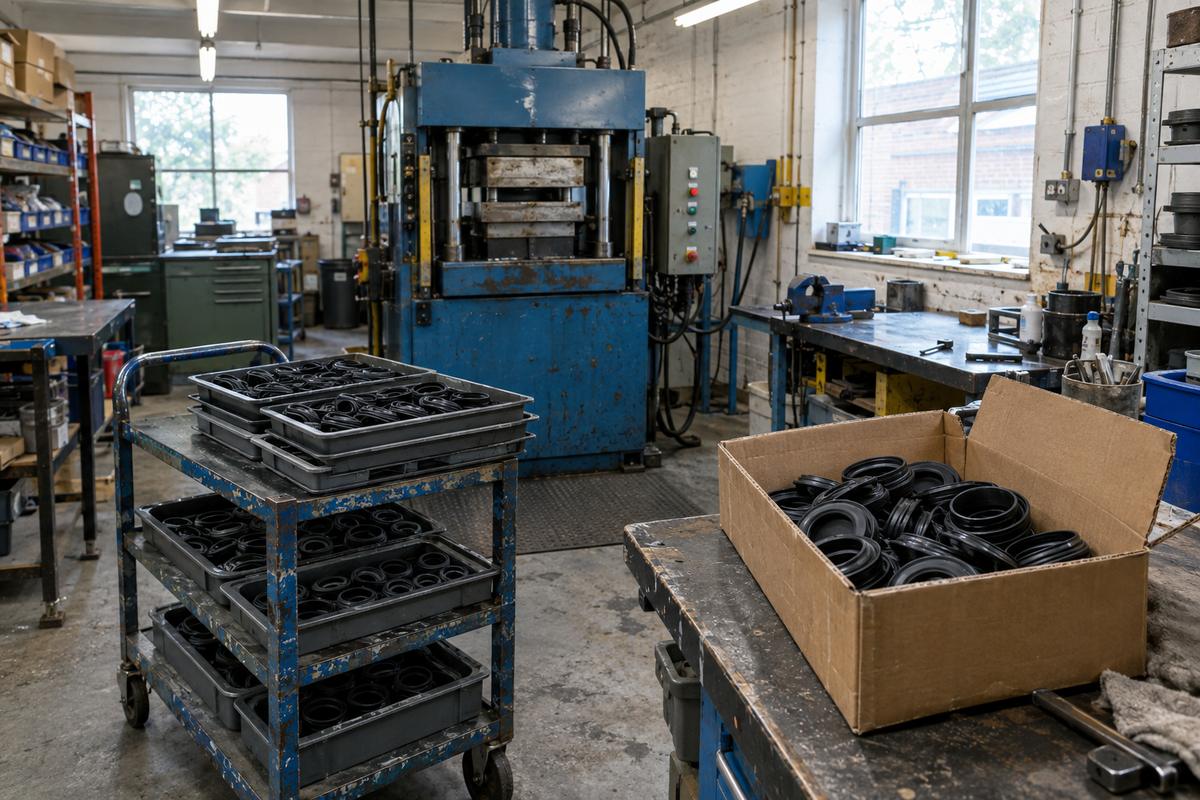
Unit cost was within a few percent of the European supplier — competitive, but not the story. The story was working capital: safety stock dropped by roughly two-thirds, freeing meaningful capital in the tier-2's balance sheet. And the tier-1 stopped seeing stock-outs on the tier-2's shipments.
The tooling investment recovered inside the first year through the inventory reduction alone. Ongoing savings continue year over year.
This project was less about manufacturing sophistication and more about matching a UK supply model to a UK build cadence. Straightforward, but valuable.
“We stopped carrying eight weeks of stock. The tier-1 stopped complaining about our OTIF. Both from moving the tool eighty miles.”
Services used
Silicone and rubber gaskets moulded to your drawing, in the grade and hardness your sealing job actually needs. Enclosure gaskets, static fluid…
See the serviceSolid silicone or rubber pre-formed, loaded into a heated steel tool, and pressed under cure. Sensible tooling cost, thousands of parts per tool, and…
See the serviceFor volumes measured in the hundreds or low thousands per batch, released on your schedule rather than ours. Bridge tooling, dedicated compression,…
See the serviceMore project records
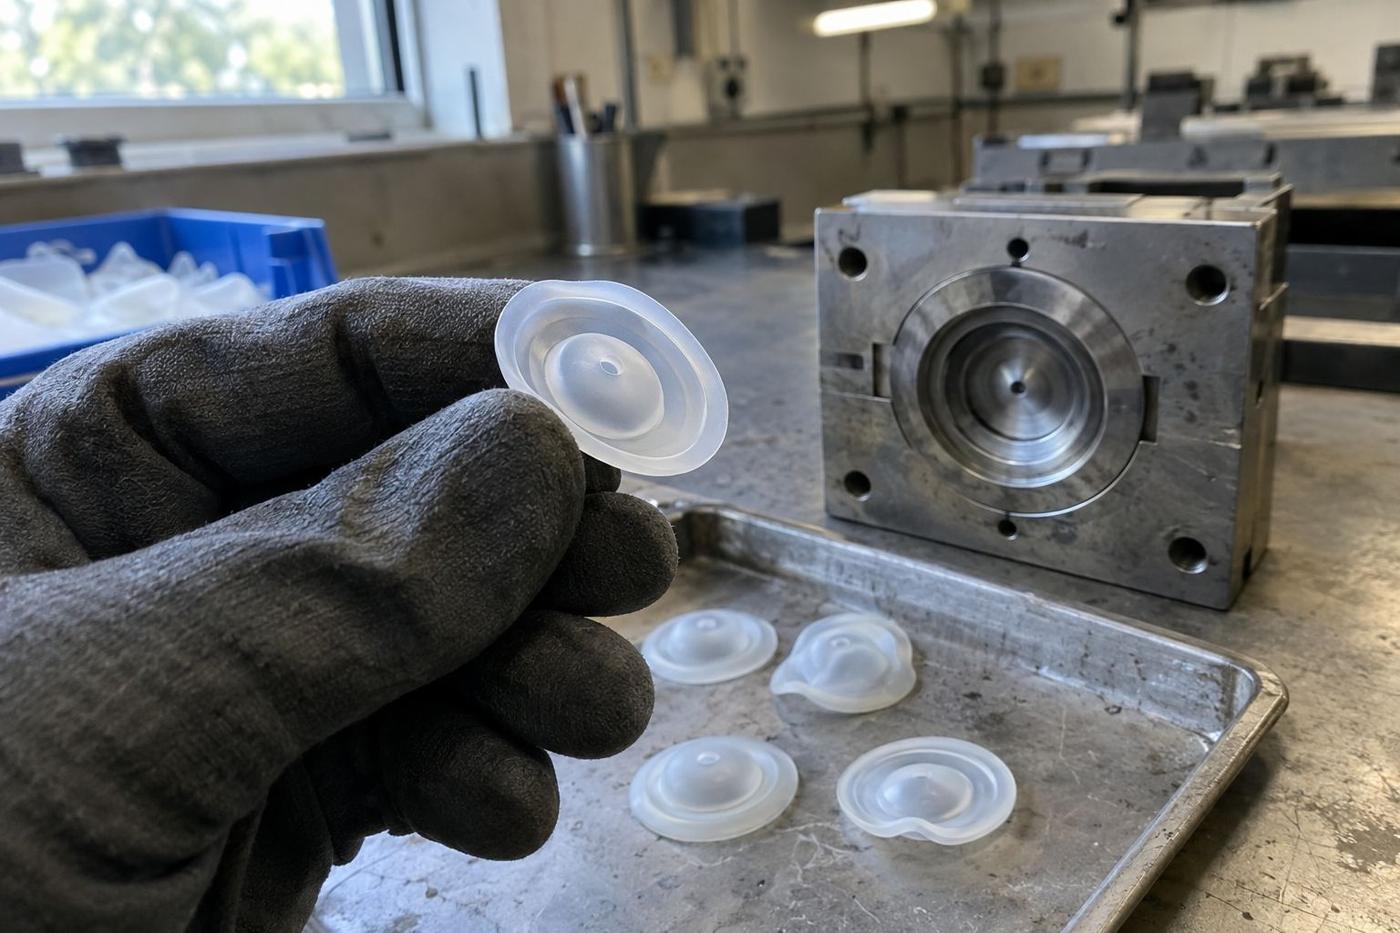
A precision-shaped silicone diaphragm that generates haptic feedback in a small consumer device. Prototype casting proved the design; production LSR held it…
Read the record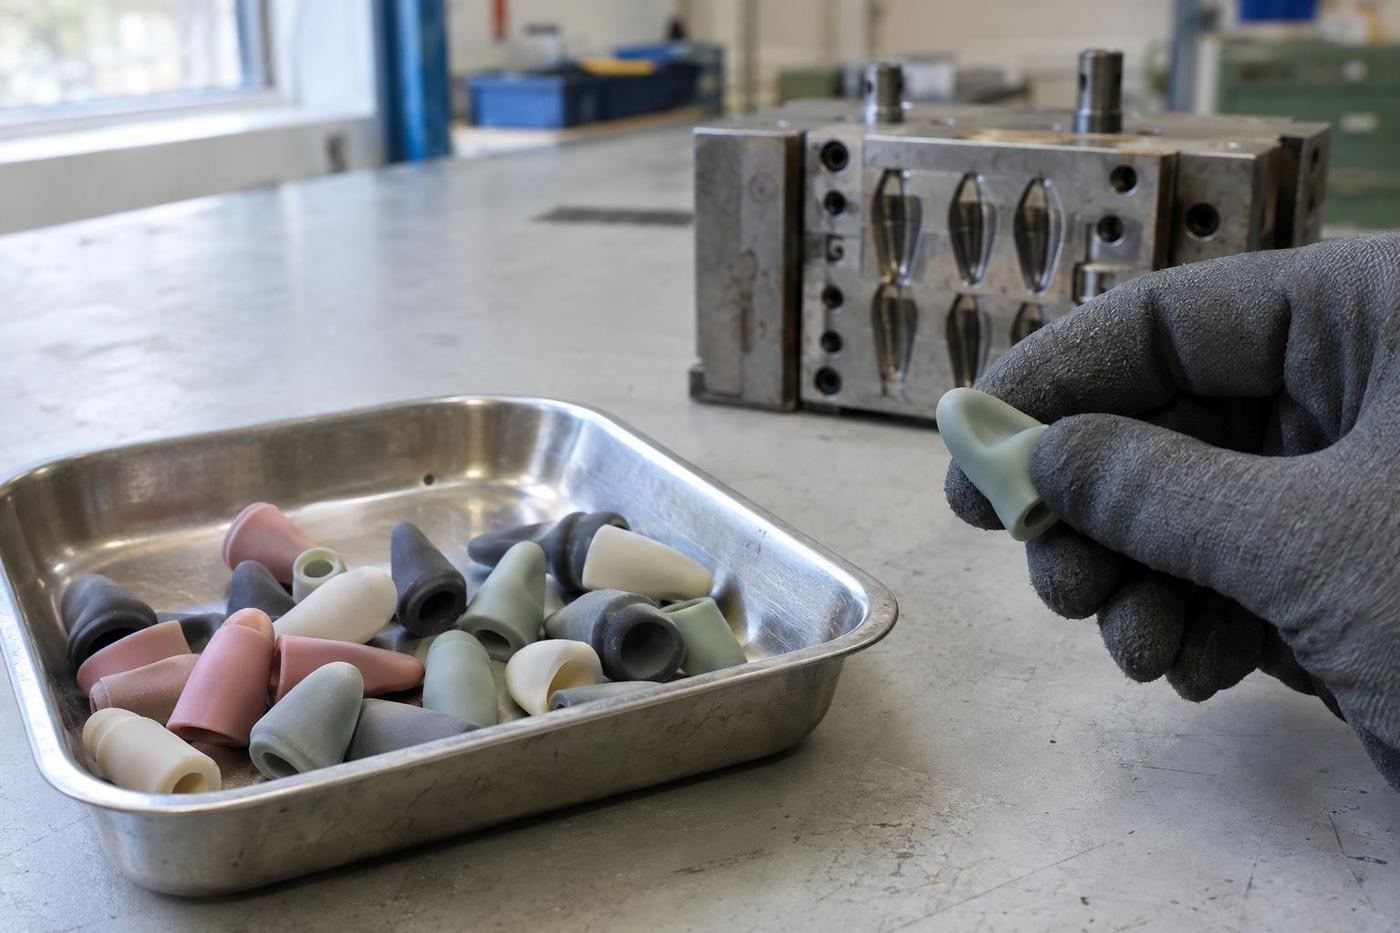
A soft silicone tip that fits on the end of a personal care device. Skin-contact, cleanable, colour-matched to the brand. Batch supply against a fluctuating…
Read the record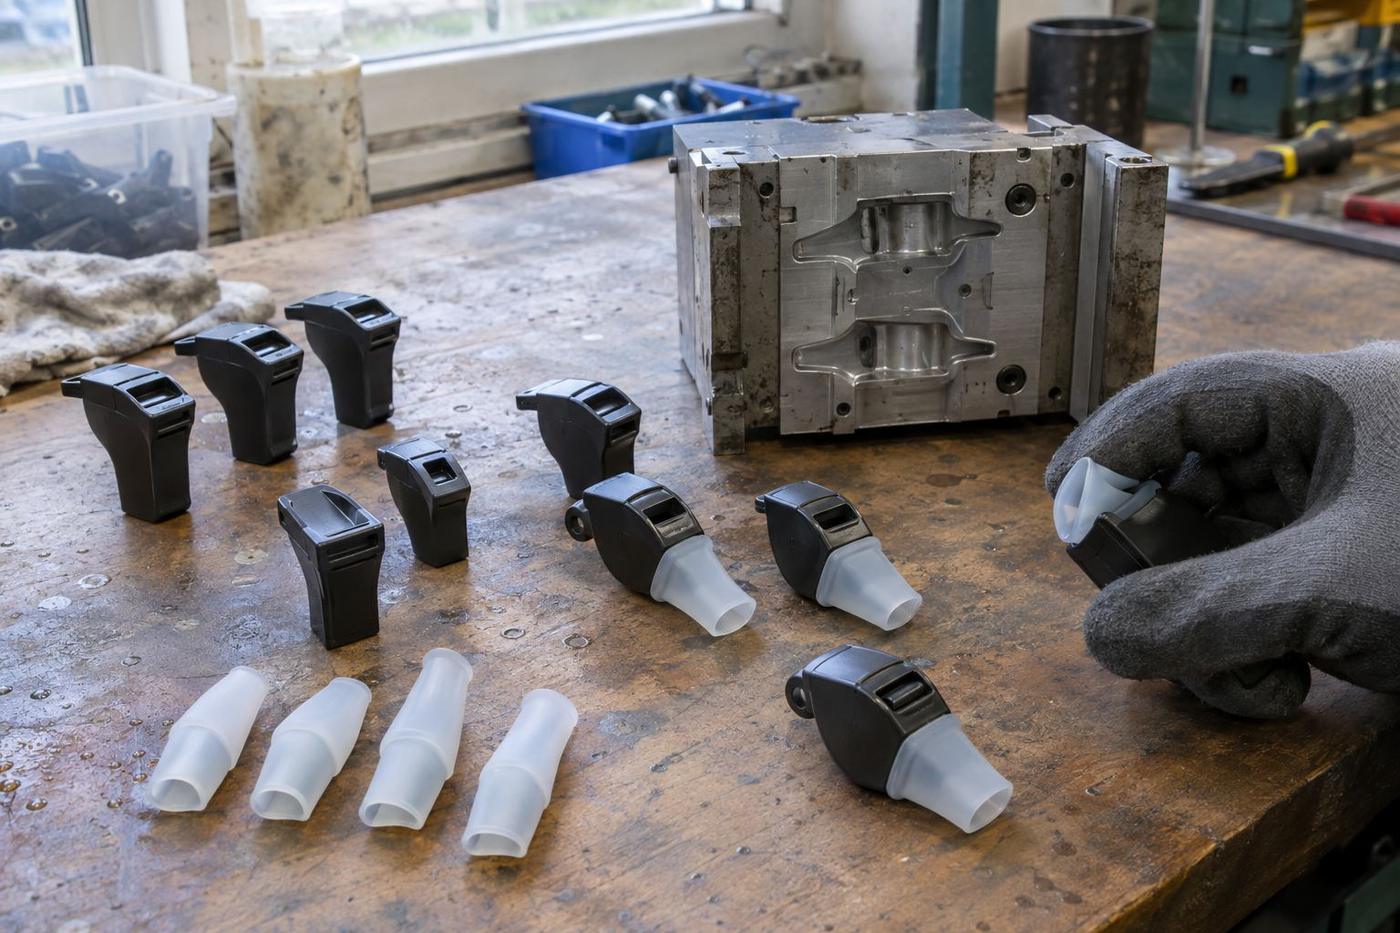
A referee whistle with a soft silicone mouthpiece bonded to a rigid plastic body. Not glamorous; used in cold weather, wet weather, and everything else. It had…
Read the recordNext step
The commercial shapes described in our project records are examples of what's worked, not prices we're quoting today. Every programme sizes differently based on part geometry, annual volume, material family and paperwork requirements.
For a first conversation about whether we'd be the right supplier for your part, send a drawing or a sample with your rough annual volume. That's enough to know if the fit is real.
Get in touch
Rough annual volume, target unit price, and any deadlines. That's enough to work out whether compression, LSR injection or something else is the right tool.
Real people, a real workshop
No call centre and no middlemen. When you contact TCI Products, you speak to the team who design, build and check your mould.



 Thomas LaneManaging Director
 George PrestonDesign & Project Manager
 Kelly BallingerHead of Partnerships
 Jim AndertonProduction Manager
 TheodoreEmployee Welfare