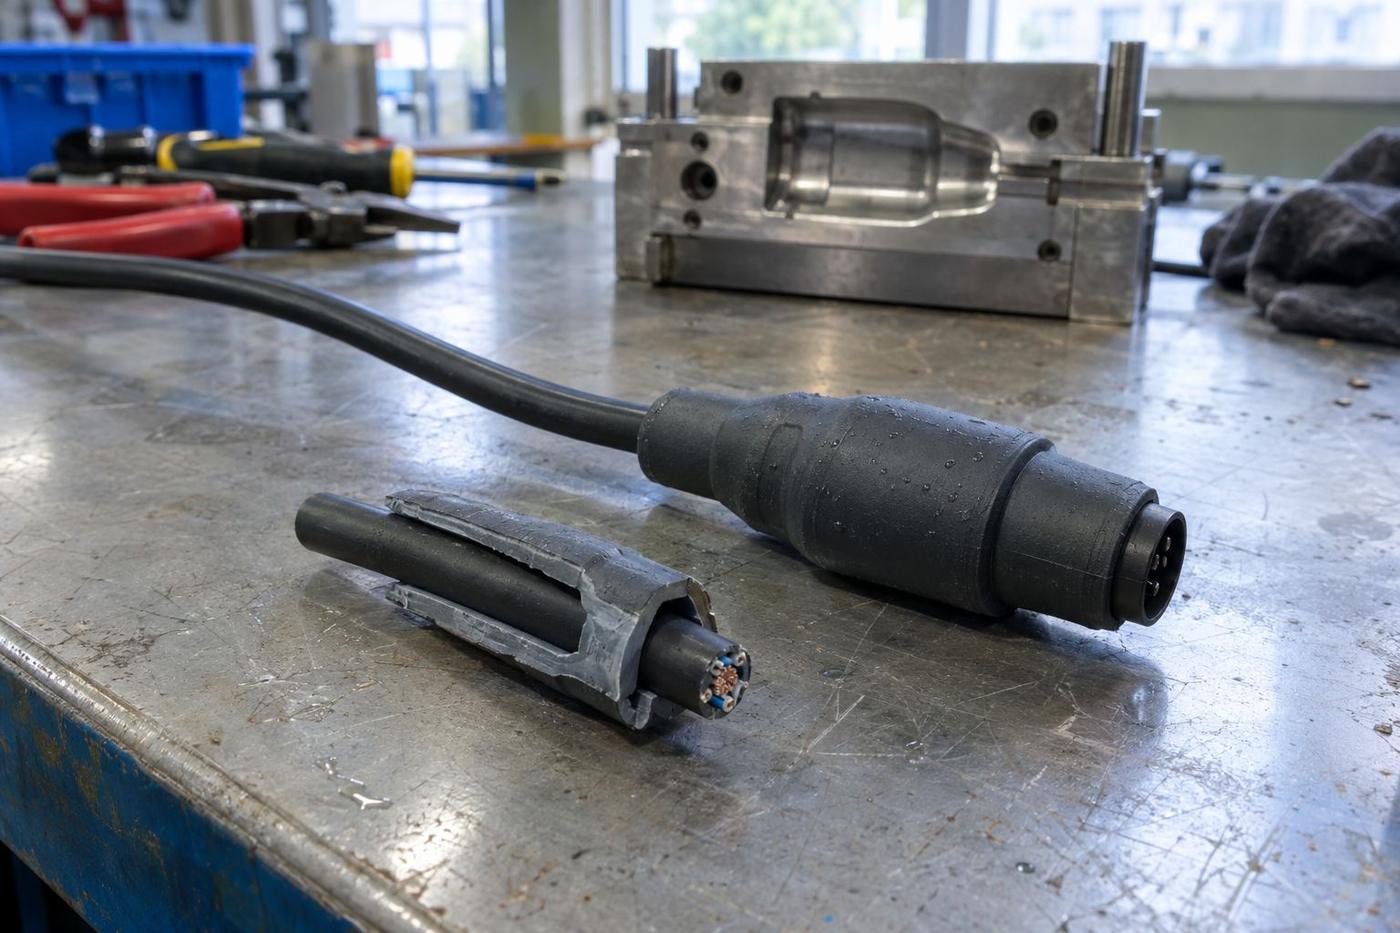
Cable and connector overmoulding
The point where a cable enters a connector or device is where most cables fail. An overmoulded silicone body seals that point, spreads the bending…
See the serviceProject record · Marine equipment · Cable overmould
Salt water was finding its way along the cable jacket and into the connector. We replaced a potted joint and heat-shrink with a single silicone overmould designed to grip the jacket.
The brief
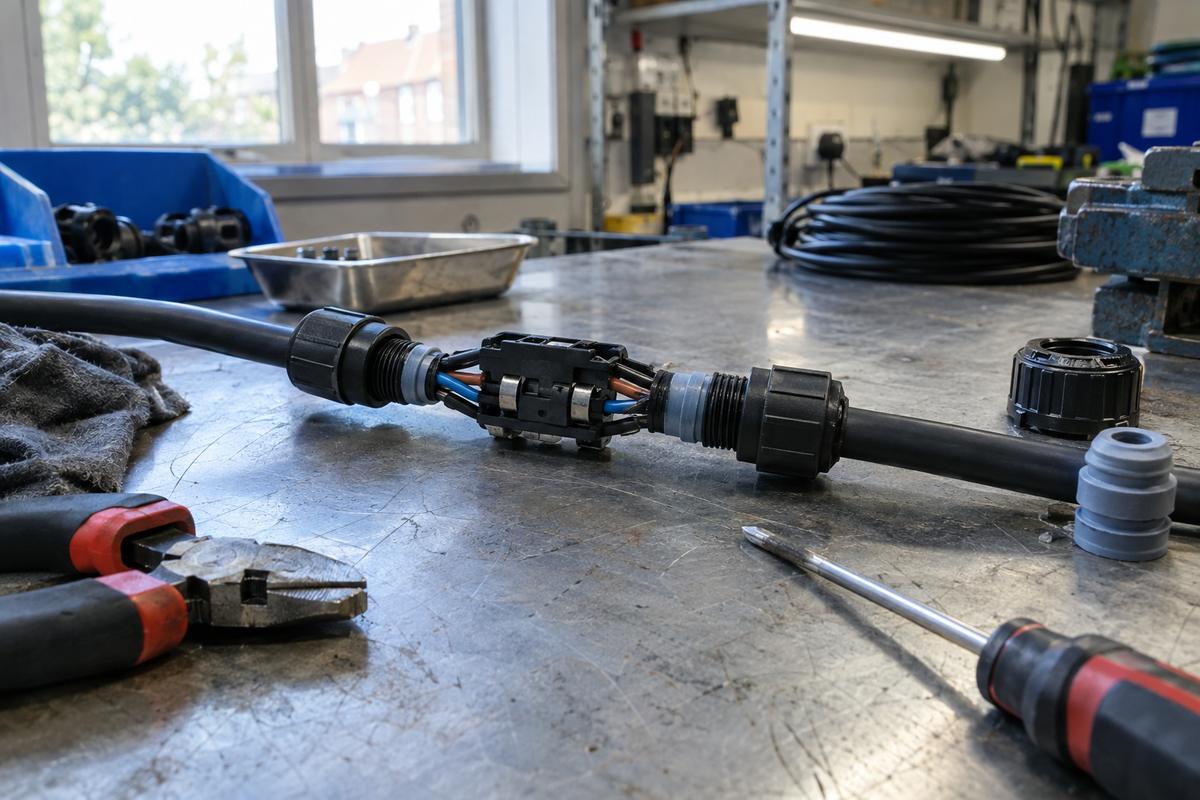
A UK maker of marine monitoring equipment had a connector on a sensor cable that sat permanently in seawater. Field returns showed corrosion inside the connector body.
The existing design used a potted joint covered with heat-shrink tubing, done by hand. Water was wicking along the cable jacket under the heat-shrink and reaching the pins.
They asked us whether an overmould could seal the joint more reliably and reduce the hand work.
The problem
Heat-shrink sealed well to itself but not reliably to the cable jacket, especially after temperature cycling. The potting compound sealed the pins but left a path along the jacket.
The fix was to bond and grip the jacket directly, over a long enough length to stop wicking, and to seal the connector body in the same moulding.
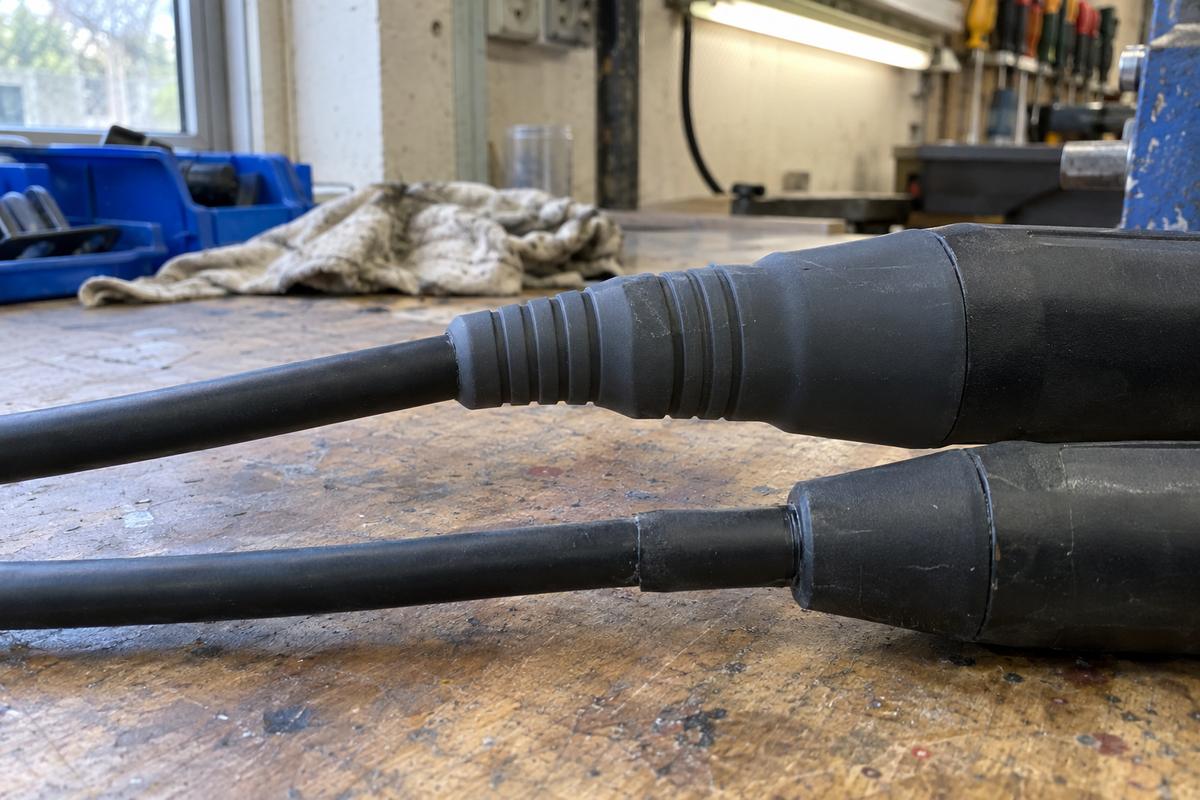
We proposed a silicone overmould with a primed jacket, a series of moulded grip rings and a tapered strain relief.
What we changed
A modest design change with a big effect on reliability.
The cable jacket was cleaned and primed over the sealing length.
Moulded internal rings compress onto the jacket to block water paths.
A tapered boot spreads bending load away from the joint.
Grade and cure chosen to protect the connector and cable.
Early samples were cut open and pressure tested.
Continuity and sample pressure checks on every batch.
The commercial shape
The overmould tool was a modest investment. Removing the potting and heat-shrink steps reduced assembly labour, and the field return rate for water ingress fell away.
The customer's own team now fits connectors to cable and sends assemblies to us for overmoulding in regular batches.
“The overmould made the connector the most reliable part of the system instead of the weakest.”
Services used
The point where a cable enters a connector or device is where most cables fail. An overmoulded silicone body seals that point, spreads the bending…
See the serviceWrapping a sensor, board or cable joint in silicone protects it from water, dust, vibration and hands. Done badly, it cracks solder joints or cooks…
See the serviceSilicone or rubber moulded directly onto a pre-made substrate — a plastic housing, a metal insert, a printed circuit assembly — so the finished part…
See the service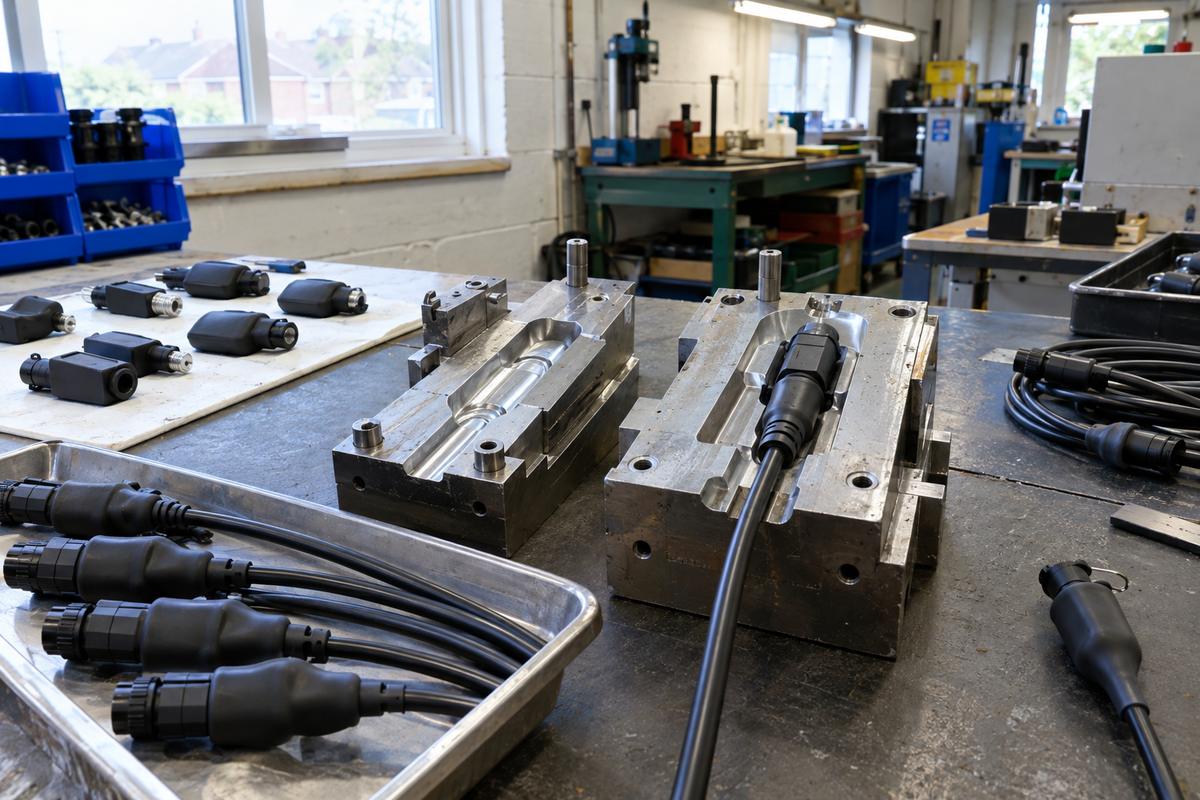
More project records
A long-standing diaphragm supplier had stopped supplying and the replacement parts from elsewhere were failing early. We re-tooled the diaphragm in compression…
Read the record
Three separate parts, bonded together by hand, kept failing the drop test at the bond line. We moved the assembly to a single overmoulded part. The bond became…
Read the record
A sealing gasket for a housing on a device that gets held all day. Compression-moulded worked, but every part needed a hand-trim on the sealing face. At…
Read the recordNext step
The commercial shapes described in our project records are examples of what's worked, not prices we're quoting today. Every programme sizes differently based on part geometry, annual volume, material family and paperwork requirements.
For a first conversation about whether we'd be the right supplier for your part, send a drawing or a sample with your rough annual volume. That's enough to know if the fit is real.
At a glance
How overmoulding works
Swipe to see the whole diagram
Get in touch
Rough annual volume, target unit price, and any deadlines. That's enough to work out whether compression, LSR injection or something else is the right tool.
Real people, a real workshop
No call centre and no middlemen. When you contact TCI Products, you speak to the team who design, build and check your mould.



 Thomas LaneManaging Director
 George PrestonDesign & Project Manager
 Kelly BallingerHead of Partnerships
 Jim AndertonProduction Manager
 TheodoreEmployee Welfare