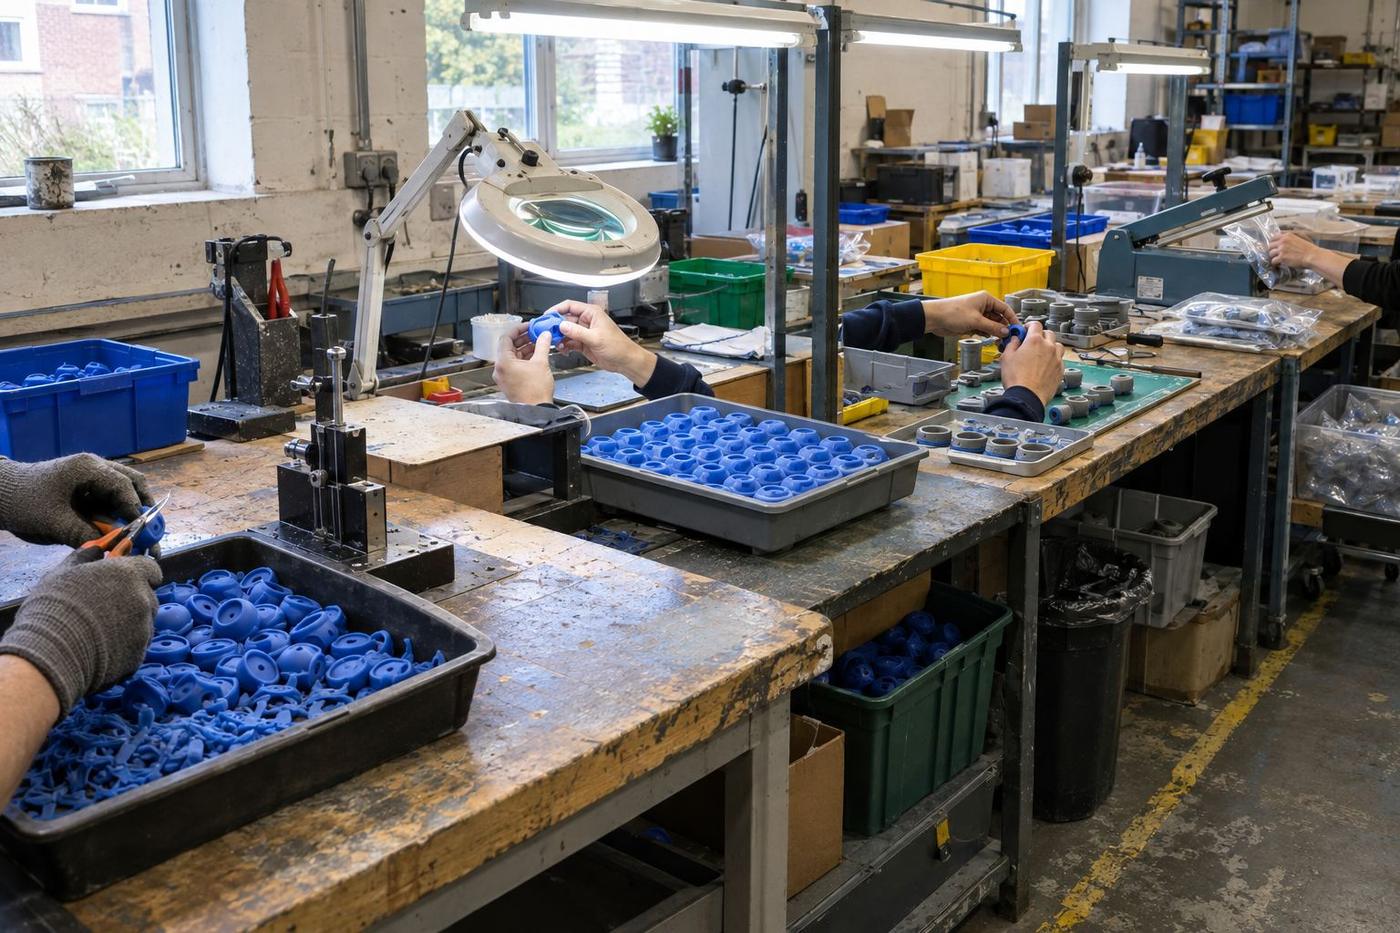
Cryogenic deflashing
Flash is the thin skin of material left at the parting line. Cryogenic deflashing freezes it brittle and knocks it off, leaving clean edges…
Open this variantOEM route · what happens after the press opens
Deflash, trim, print, bond, assemble, inspect and pack. Everything that has to happen between the press opening and the part being ready for your assembly line, done in one place, on documented processes.
Why this matters
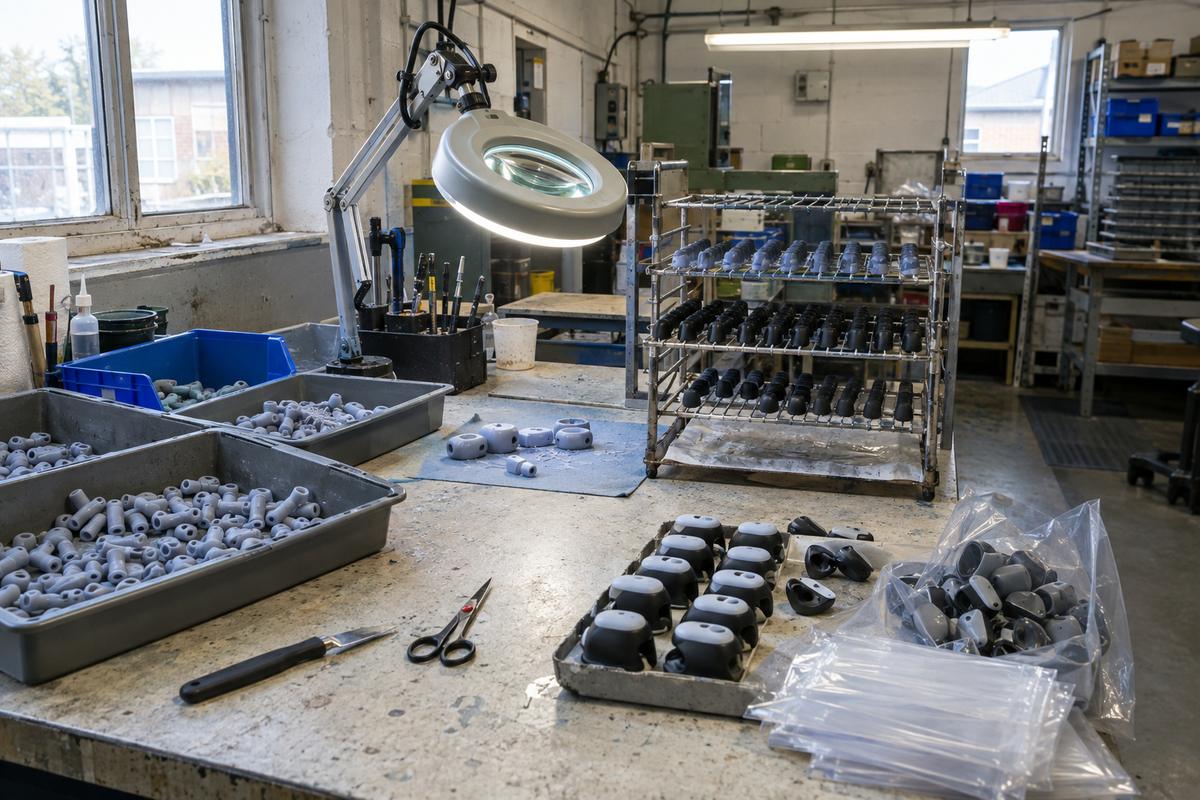
Very few silicone parts come off the press ready for a customer to see. Most need some combination of trim, print, coating, bonding, sub-assembly or inspection before they're ready for your line. Where that work happens shapes both the cost and the reliability of the finished part.
For most parts we mould, the finishing happens here rather than at your end. That has two advantages: we know the parts, we know the material, and we can catch a mould-side issue before it turns into a finishing-side scrap rate. And it collapses the paperwork — one supplier, one batch record, one shipment.
The finishing capability covers cryogenic and hand deflashing, silicone-compatible pad-printing, UV coating for wear resistance, adhesive bonding for sub-assembly, ultrasonic and RF welding for silicone-to-silicone joints, and full sub-assembly with your other components if you'd rather ship us the parts than assemble at your end.
For everything, the process is documented: what happens, in what order, on what fixture, with what material batch. The batch record covers the moulding and the finishing together, so your incoming inspection sees a single traceable job.
Drill down
Each variant has its own page with the specifics: where it fits, how we run it and what to send us.
Flash is the thin skin of material left at the parting line. Cryogenic deflashing freezes it brittle and knocks it off, leaving clean edges…
Open this variantLogos, legends, part numbers and batch codes. Marking silicone takes the right inks, surface preparation and curing, otherwise it rubs off.
Open this variantParts arriving checked, counted and packed the way your line uses them save your goods-in team hours.
Open this variantWhat finishing covers
Cryogenic tumble for higher volumes, hand deflash for parts where the finish criteria are cosmetic or sealing-critical. Both routes documented and inspected.
Silicone-compatible pad-printing for graphics; UV coating for wear or feel; laser marking for permanent codes. All processes tested for adhesion and durability before scale-up.
Sub-assembly with metal, plastic or PCB components you supply. Bonded, welded, mechanically assembled, or a combination — packaged as finished sub-units for your line.
How finishing runs
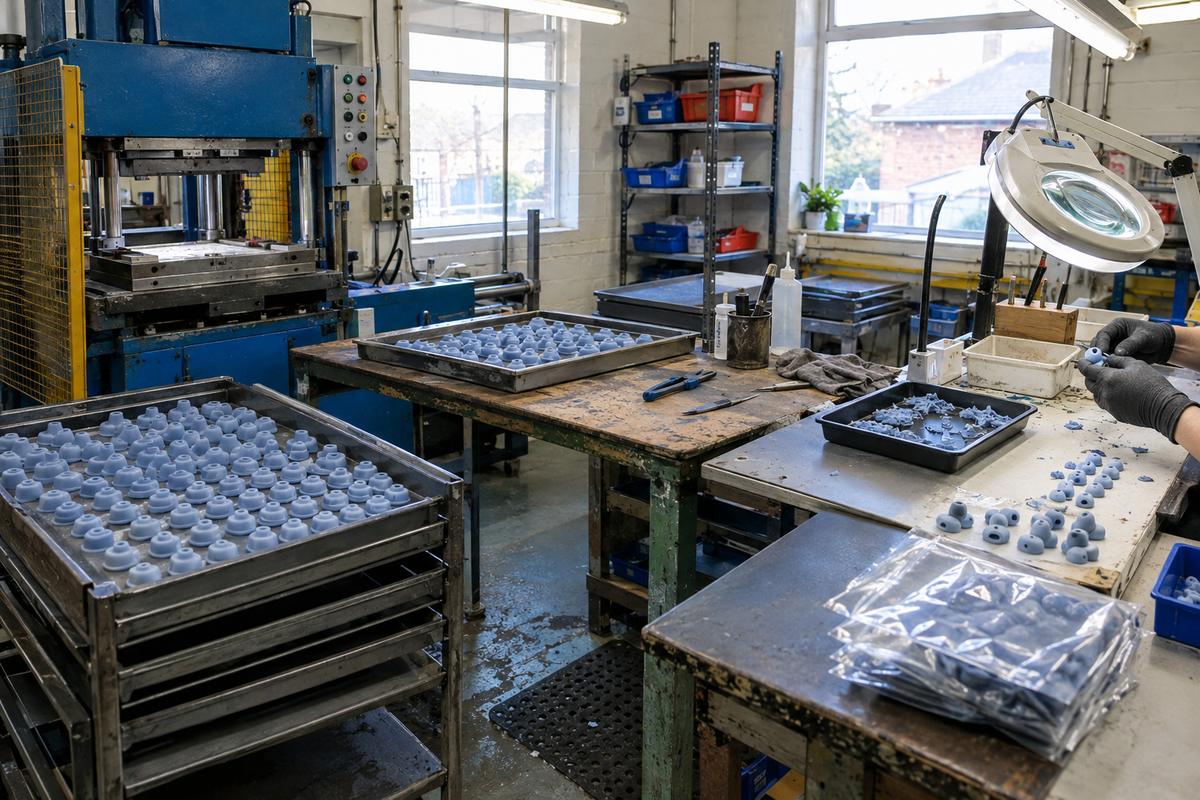
Finishing runs in a cell right next to the moulding cell. Parts flow directly through rather than being packed, shipped and re-received.
Once the mould run has produced a good first-off, we finish a sample through the full route. You sign off the finish spec against a physical part, not just against a drawing.
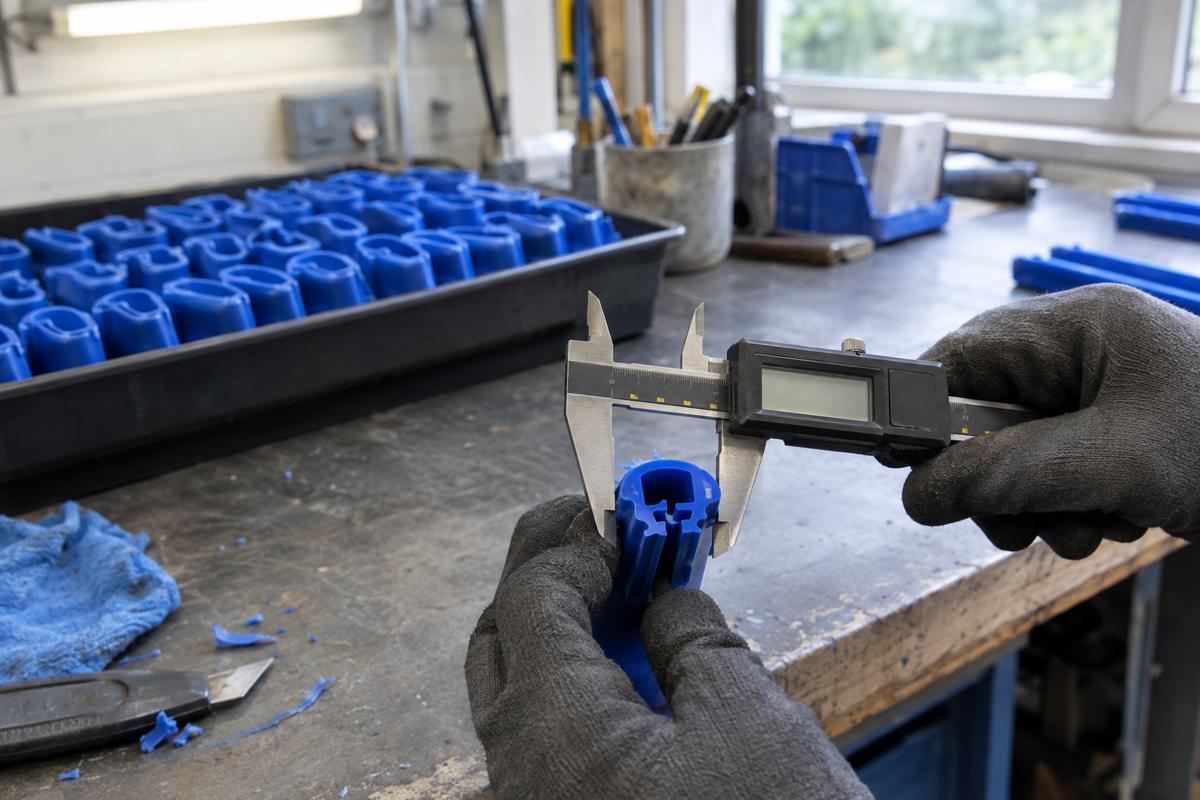
Deflash by the agreed route. Cosmetic or sealing faces inspected under magnification; internal or hidden faces inspected to standard tolerance.
Any decoration or coding applied. Adhesion checks on every batch; UV cure exposure monitored on coated parts.
Bonded, welded or mechanically assembled with the components you've supplied. Fixtures held on-site; assembly documented against the drawing.
Full-spec inspection at end of line. Packed to your spec — trays, bags, kits — and shipped with the batch record.
To quote it
Cosmetic acceptance criteria, visible surfaces, forbidden marks. Ideally with a reference part or a golden sample from an earlier run.
Graphics, colours, coating layers, and whether the finish needs to survive specific durability tests at your end.
What components come from you, what we source. What the assembled unit needs to look and feel like when you pick it up on your line.
Finishing capacity is planned alongside moulding capacity. If volumes are lumpy, we'll model both against realistic lead time.
Related routes
Silicone products moulded, finished, packaged and labelled to your brand — ready to ship into your retail, e-commerce or wholesale channel. Your…
Read moreFor volumes measured in the hundreds or low thousands per batch, released on your schedule rather than ours. Bridge tooling, dedicated compression,…
Read moreSilicone parts for products people wear, hold, or wipe every day — ear tips, straps, grips, sleeves, applicators. Made to a colour and feel you sign…
Read moreGet in touch
Rough annual volume, target unit price, and any deadlines. That's enough to work out whether compression, LSR injection or something else is the right tool.
Real people, a real workshop
No call centre and no middlemen. When you contact TCI Products, you speak to the team who design, build and check your mould.



 Thomas LaneManaging Director
 George PrestonDesign & Project Manager
 Kelly BallingerHead of Partnerships
 Jim AndertonProduction Manager
 TheodoreEmployee Welfare