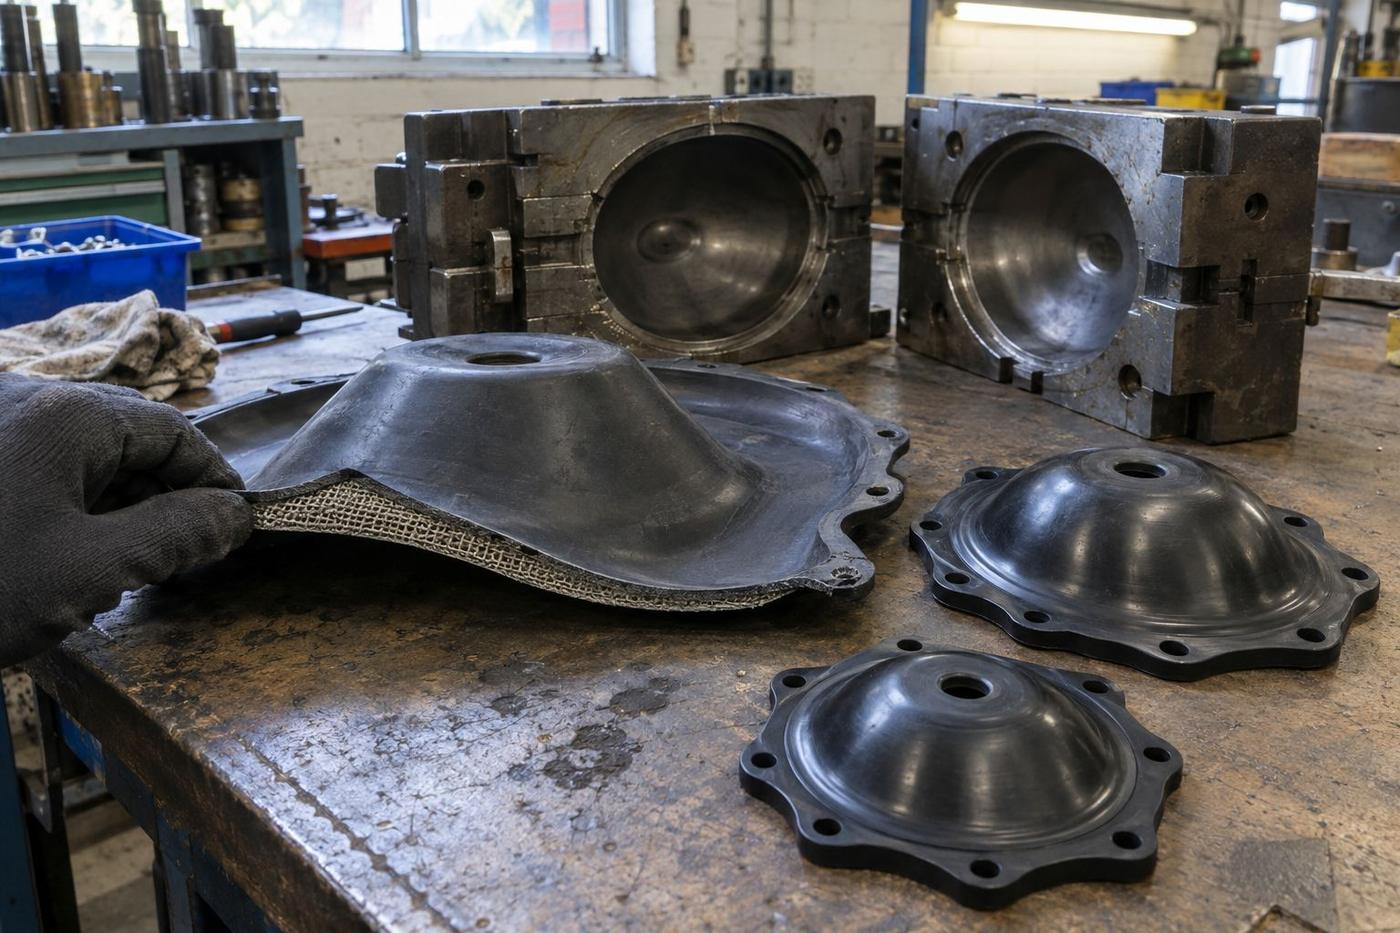
Valves and diaphragms
A valve is judged on one thing: does it open and close the way it's supposed to, every time. That comes down to wall section, material hardness and…
See the serviceProject record · Industrial equipment · Compression
A long-standing diaphragm supplier had stopped supplying and the replacement parts from elsewhere were failing early. We re-tooled the diaphragm in compression with a properly positioned fabric layer.
The brief
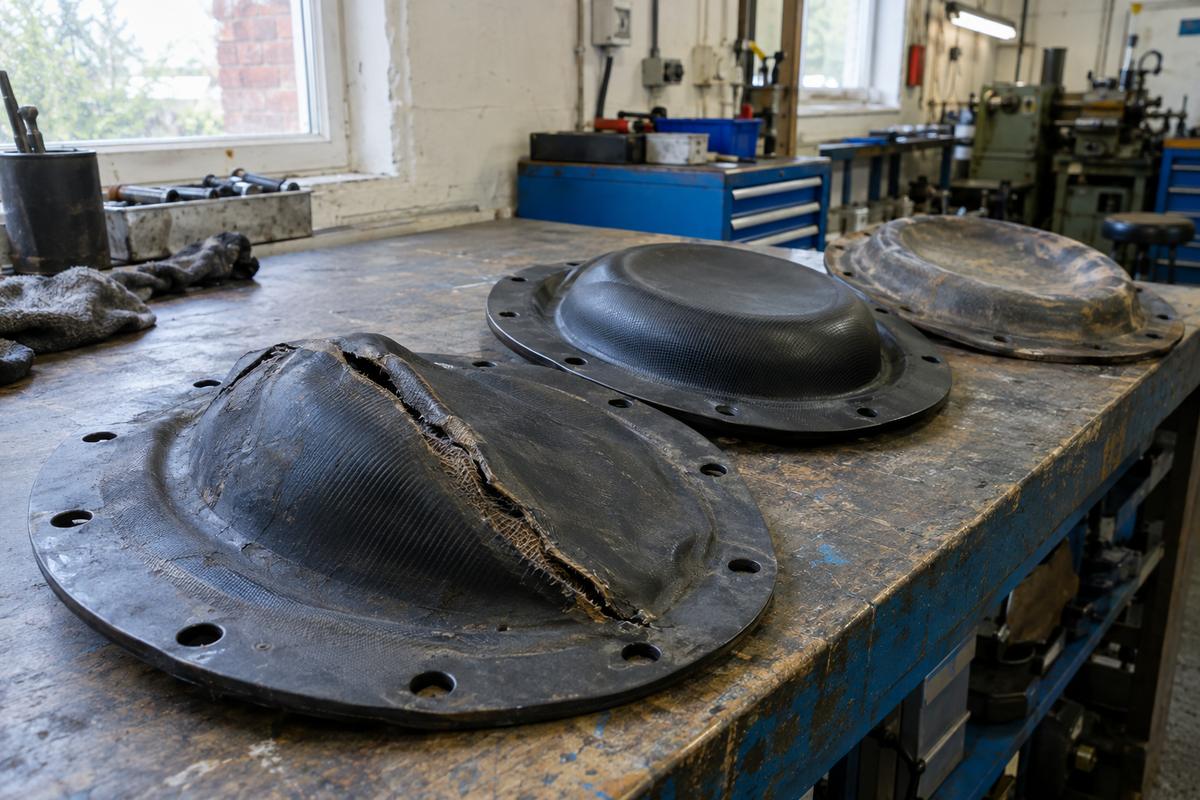
A UK maker of industrial dosing pumps relied on a fabric-reinforced rubber diaphragm. Their long-standing supplier had closed, and the alternative parts they'd sourced were failing much earlier than the originals.
They brought us samples of both: original parts that had run for years and replacement parts that had split.
The ask was simple: make diaphragms that last like the originals.
The problem
Cutting open failed replacement parts showed the fabric layer was off-centre, leaving a thin rubber section on one side that cracked under repeated flexing.
The original parts had the fabric held centrally throughout the flexing zone.
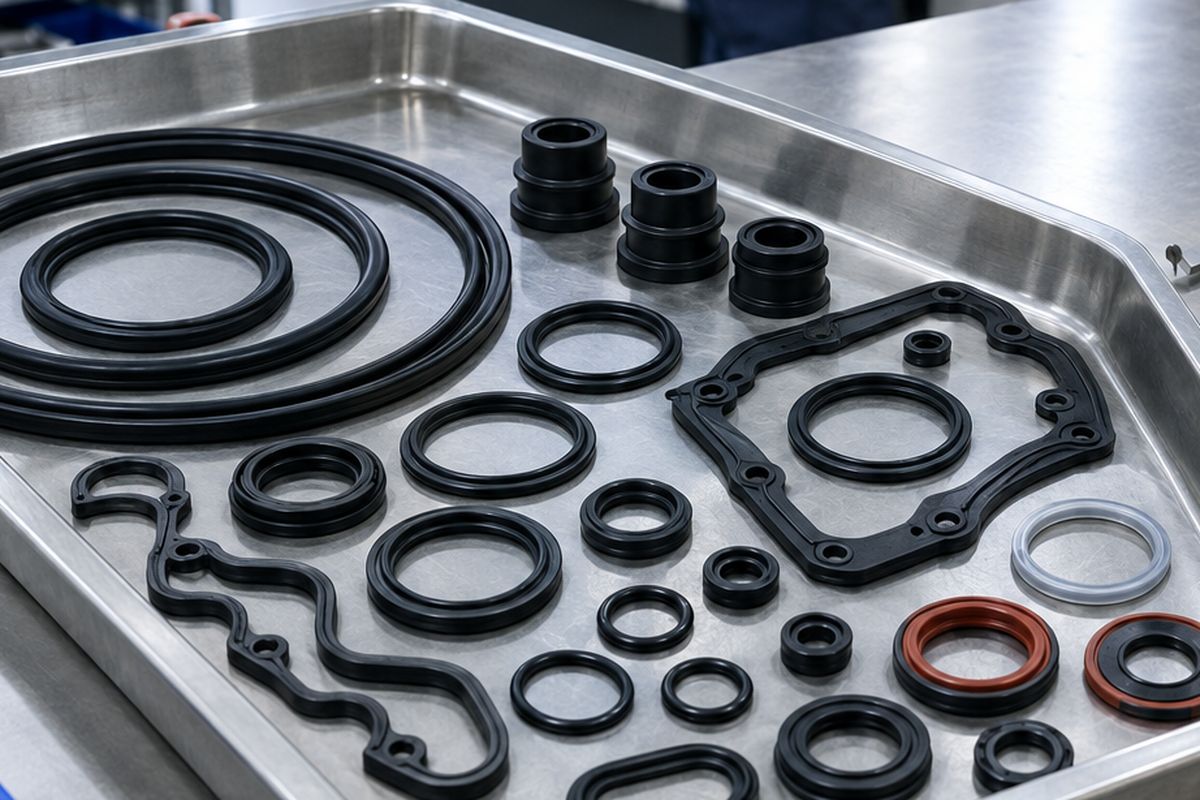
The fix was a compression tool and loading method that located the fabric precisely and kept it there during cure.
What we changed
Most of the work was in the tool and the loading sequence.
Original and failed parts were sectioned and compared.
A compound chosen for the pumped media and flex life.
Tool features and pre-forms that hold the fabric centrally.
A documented sequence for pre-forms and fabric.
Sample parts sectioned each batch to check fabric position.
Samples supplied for the customer's pump life test.
The commercial shape
The new diaphragms matched the originals in the customer's life tests. The tool is held by us and runs in regular batches.
The customer now has documented compound and process records, which they didn't have with the original supplier.
“We didn't need a cheaper diaphragm. We needed one that lasted. Now we have it.”
Services used
A valve is judged on one thing: does it open and close the way it's supposed to, every time. That comes down to wall section, material hardness and…
See the serviceA diaphragm flexes thousands or millions of times. Its life depends on material, section and how evenly it was moulded.
See the servicePads, buffers, bellows, grommets and seals for machines that have to keep running. Industrial compression work is about the right compound and a part…
See the service
More project records
Three separate parts, bonded together by hand, kept failing the drop test at the bond line. We moved the assembly to a single overmoulded part. The bond became…
Read the record
A sealing gasket for a housing on a device that gets held all day. Compression-moulded worked, but every part needed a hand-trim on the sealing face. At…
Read the record
Small, soft, colour-critical parts that customers hold to their heads for hours. Hand-cast pilot samples proved the design; production tooling had to hold the…
Read the recordNext step
The commercial shapes described in our project records are examples of what's worked, not prices we're quoting today. Every programme sizes differently based on part geometry, annual volume, material family and paperwork requirements.
For a first conversation about whether we'd be the right supplier for your part, send a drawing or a sample with your rough annual volume. That's enough to know if the fit is real.
At a glance
How overmoulding works
Swipe to see the whole diagram
Get in touch
Rough annual volume, target unit price, and any deadlines. That's enough to work out whether compression, LSR injection or something else is the right tool.
Real people, a real workshop
No call centre and no middlemen. When you contact TCI Products, you speak to the team who design, build and check your mould.



 Thomas LaneManaging Director
 George PrestonDesign & Project Manager
 Kelly BallingerHead of Partnerships
 Jim AndertonProduction Manager
 TheodoreEmployee Welfare