Sequence
Plan bend order so flanges clear the tooling.
Manufacturing services · Chapter D · Method 23
A press brake forces a punch into a V-die to bend sheet to an exact angle. Back gauges position each bend in sequence.
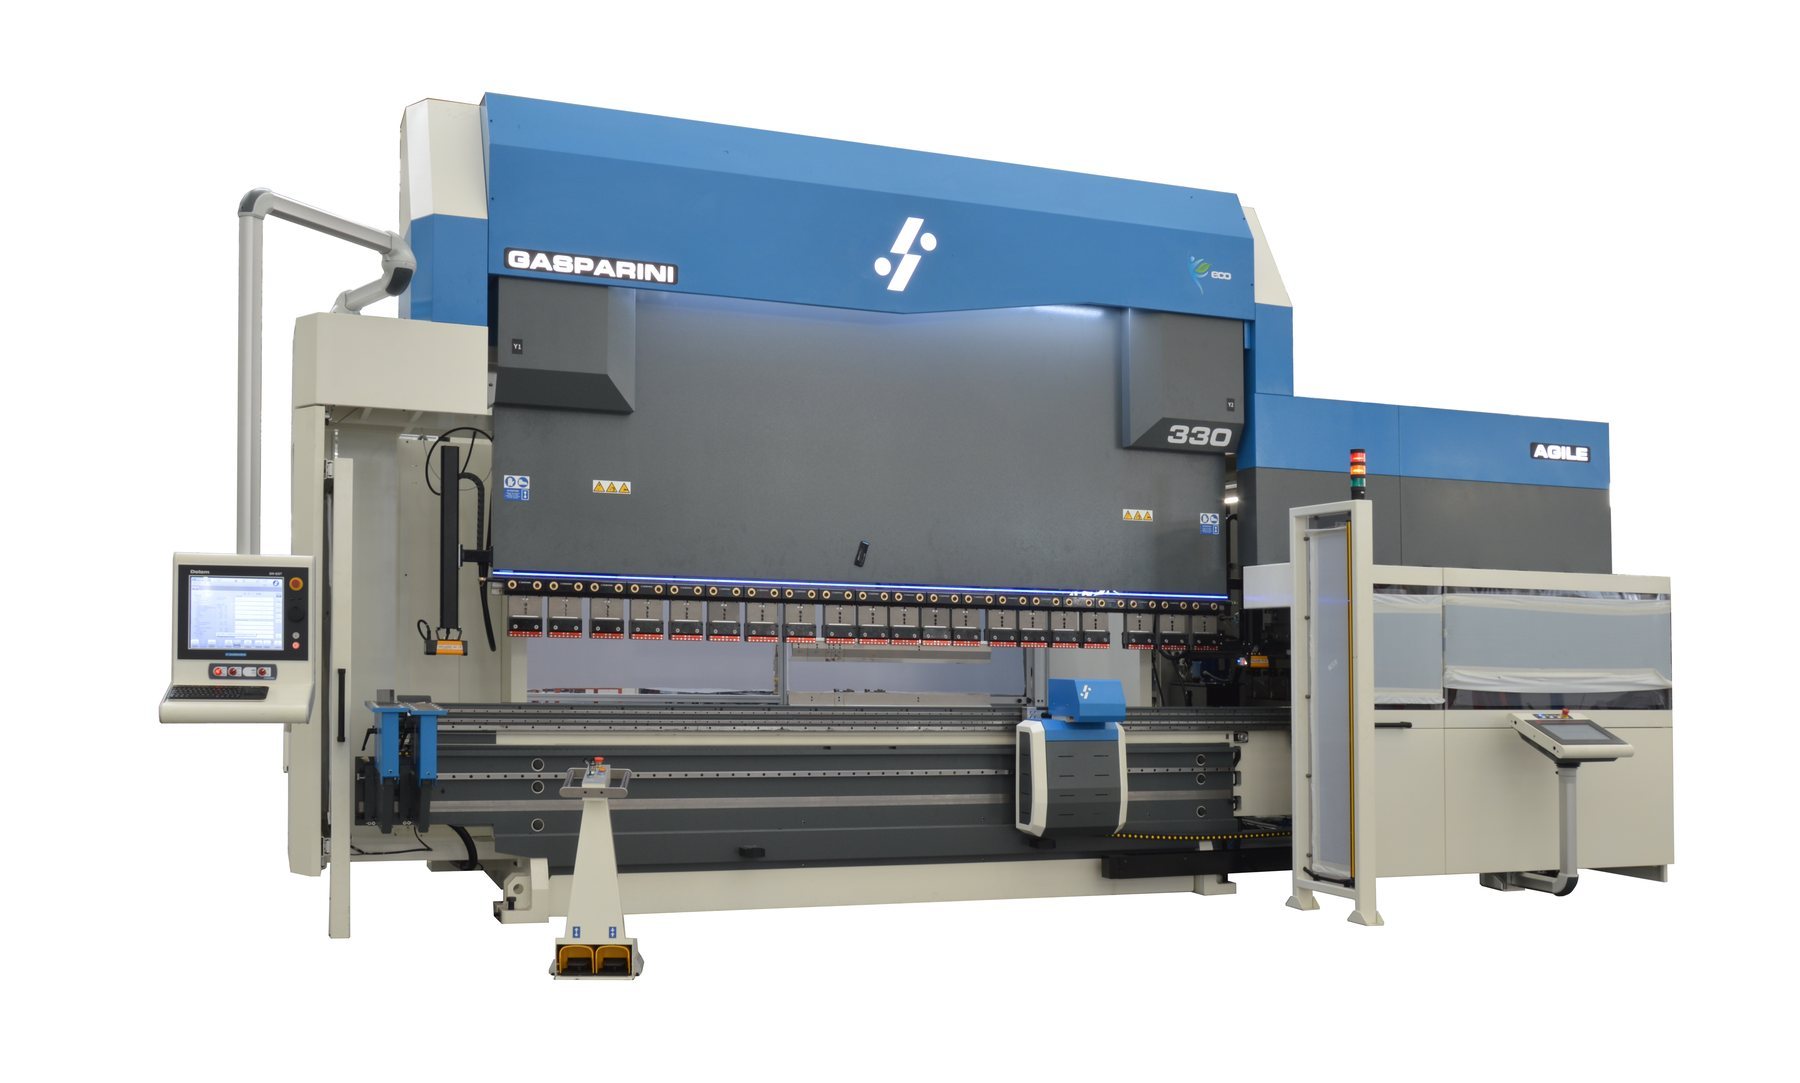
How it works
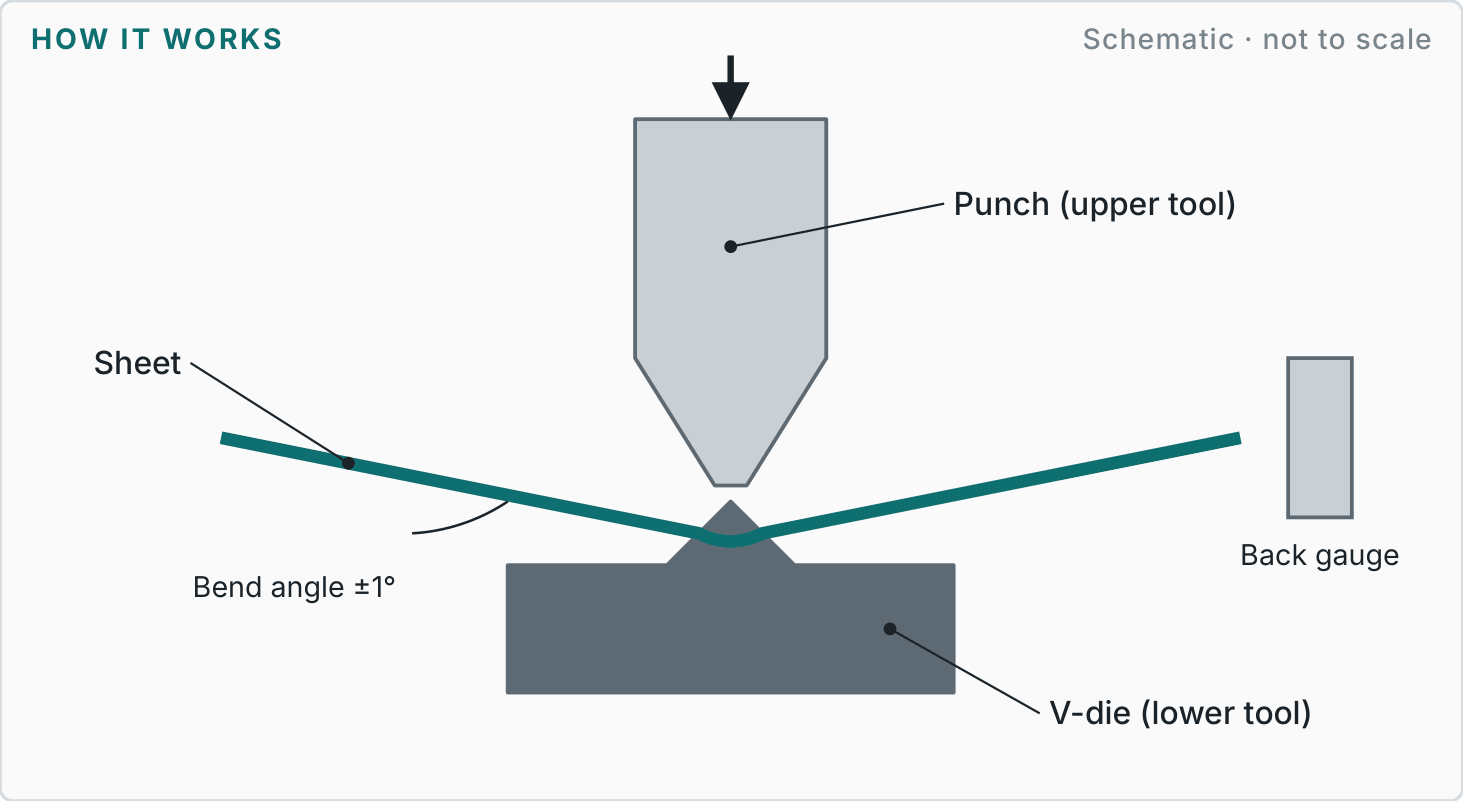
A labelled schematic of the process (not to scale), and the four steps every job goes through.
Plan bend order so flanges clear the tooling.
Back gauge positions the sheet.
Punch forms the sheet into the die.
Measure angle; adjust for springback.
Reference figures
Typical industry values to help you plan. We agree the figures for your part on the drawing.
| Materials | Mild steel, stainless, aluminium, galvanised steel and copper alloys. |
|---|---|
| Finishes | Tool marks possible on soft or polished sheet; protective film helps. |
| Design guidance |
|
| Best suited to | Brackets, channels, trays, enclosures and frames. |
| Watch-outs | Springback varies by alloy; very short flanges are hard to form. |
More in chapter D
Next step
Send a sketch, photo, sample or CAD file with your quantity and target date. We will recommend the most sensible route and explain the trade-offs before quoting.
Reference figures are typical published industry values for planning, not a guarantee; final tolerances, materials and finishes are agreed in writing for each project.